Why does compressed air leaks require systematic management?
Individual leakages appear to be small, but large plant-wide leakages increase the operation time, energy costs and maintenance burden of compressors.The establishment of repeatable inspection routes is more effective than occasional spot checks.
Create Effective Inspection
- Lines by area and equipment responsibilities
- Record sound evidence, location and priority
- Arrangement of maintenance windows with accessibility
- Rescale and maintain pre- and post-recovery records
Tracking improvements
Ongoing statistics on unclosed problems, proven repairs and duplicate locations, trend data can help engineering teams address root causes rather than repeat the same phenomenon.
Technical rationale and application objectives
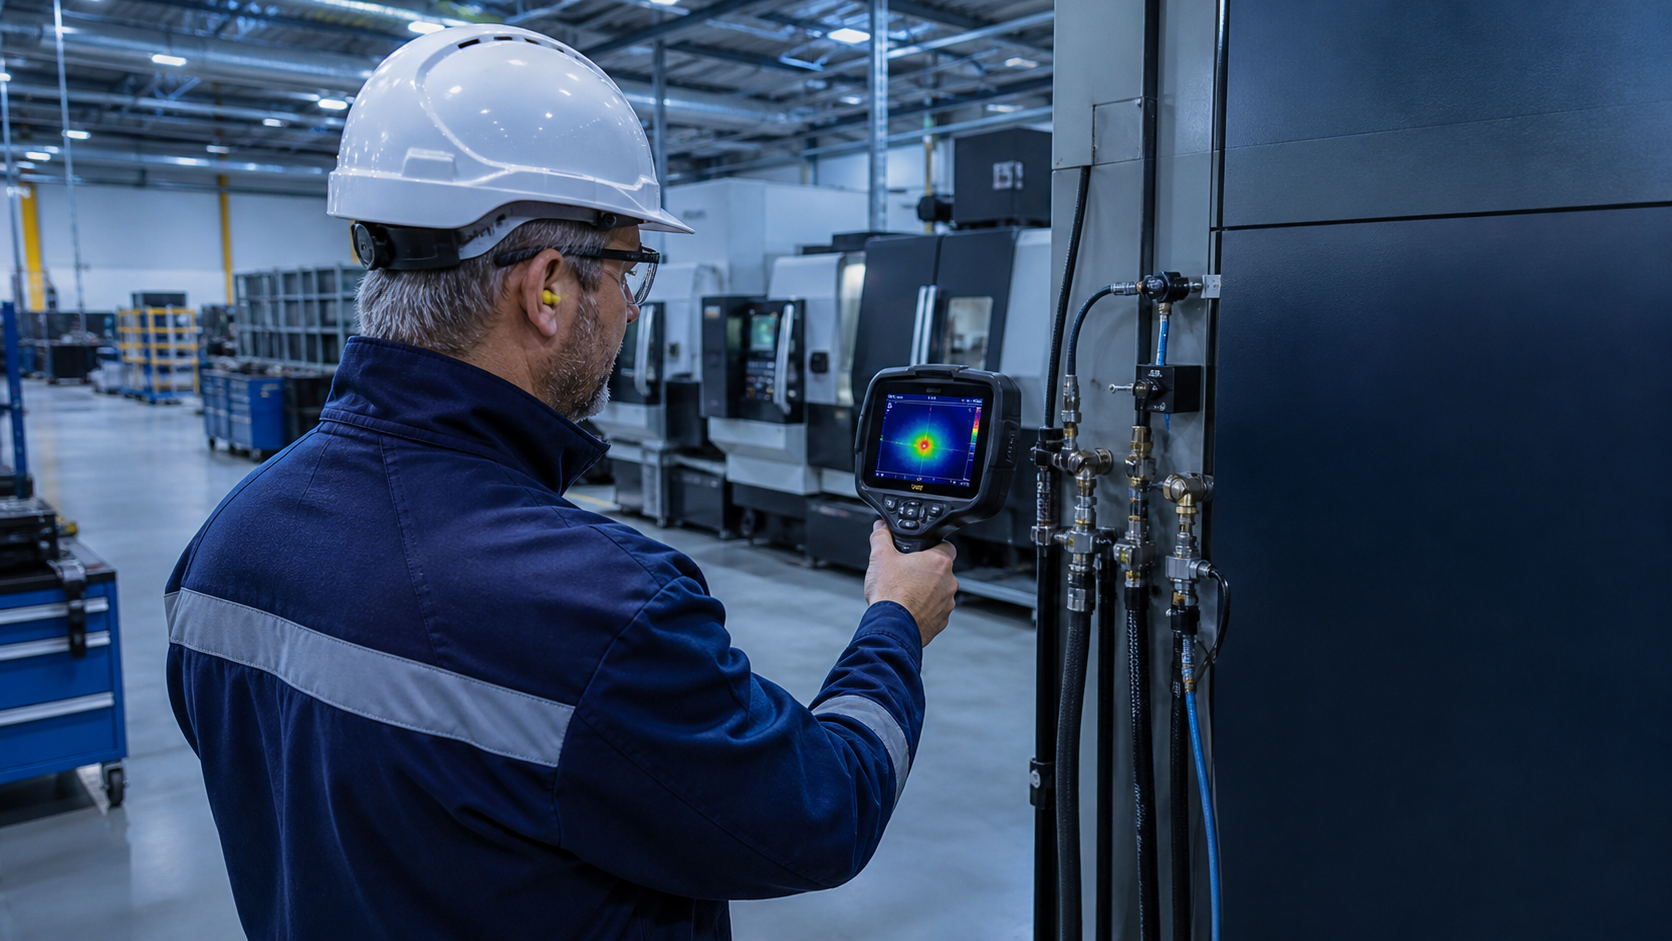
In the context of the theme “How to reduce air leaks in factories”, the field team needs to first identify the target, the accessible location, the operational state and the type of evidence to be produced.To understand practical steps to identify and eliminate air leaks.The actual test does not simply target the equipment, but combines optical imaging, acoustic positioning, operating paths and results into a reusable technical process.Information collected is of engineering value only if environmental limitations, equipment capacity and acceptance requirements are recognized prior to operations.
Prepare for testing.
Before starting work, the equipment ‘ s state, amount of electricity, surface of the probe or sensor, storage space and time date setting shall be checked, and attachments shall be selected according to the detection distance, entry size, temperature, medium and safety requirements on site.For industrial borescope, excessive tipping of the probe is to be avoided and lighting and switch function is to be confirmed;For acoustic imaging camera, environmental noise, detection frequency, distance and equipment load should be understood.Rapid validation of the images, focus, sound source localization and recording functions is completed on known targets as necessary.
On-site Operations
The detection process should be conducted on a point-by-point basis along a pre-planned route, maintaining a stable observation distance and consistent direction of the photograph.When abnormalities are detected, not only a partial picture should be kept, but also the equipment number, location, operating condition, observation angles and abnormal features should be recorded, and comparative evidence should be added to the panorama, proximate map or different frequency bands.Any uncertainty should be reconfirmed by changing angles, distances or parameters to avoid miscalculating reflection, background noise, contaminants or normal structures as defects.
data analysis and review
Once the collection has been completed, engineers will need to analyse the equipment in conjunction with historical records, process conditions and maintenance standards.Clarity does not mean that the conclusions are necessarily correct, nor does the acoustic hotspots amount to a malfunction per se, so the test evidence should be linked to location, time and operational status.(b) Discoveries affecting safety, quality or continuous production should be prioritized and re-checked;In cases of temporary non-confirmation, original documents and parameters should be retained for subsequent joint evaluation by technicians.
Development of implementable outcomes
An effective technical record should allow those who did not participate in the on-site testing to understand where the problem occurred, what the evidence was, what the level of risk was and what should be done next.It is recommended that the report retain the detection route, equipment set-up, critical photographs, basis of judgement, recommendations processed and the results of the re-examination after maintenance.Through standardized records and continuous accumulation, the enterprise can convert a single test into a trend in the state of equipment and provide a more reliable basis for preventive maintenance, spare parts planning and downtime arrangements.