Client success cases

Success cases

Real clients, real results.
0.85 mm super-spectroscope detection internal defects
Success cases

0.85 mm super-spectroscope detection internal defects

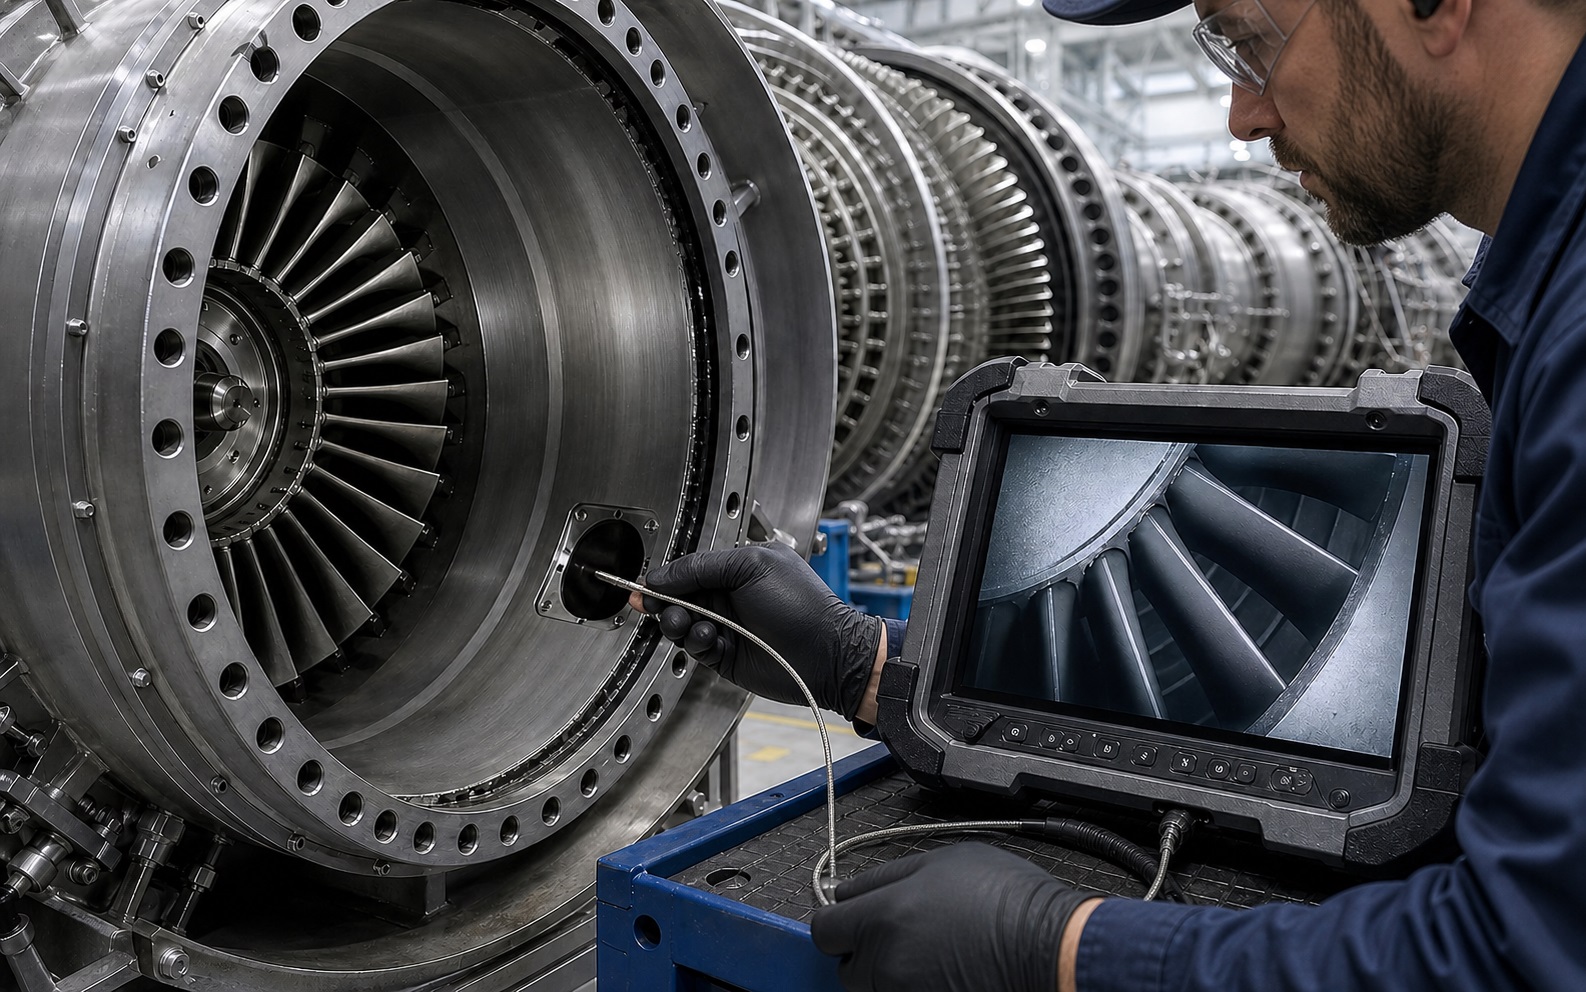
0.85 mm super-spectroscope detection internal defects Testing target. Confirms visible anomalies such as residues, constrictions, cracks, etc., in the inner narrow cavities of the precision castings, in the small stream and in the connecting areas. Test Method (c) Enter the small stream by using a super-specior lens less than 1 mm, gradually advance the probe according to the intended path, focus on the key nodes and record the location of the defects and the corresponding images. Apply Results Internal state evidence is obtained in the context of reduced dismantling and destructive inspections, and engineers may conduct further testing or maintenance of recorded locations to improve abnormality efficiency.

  • Clear detection route.
  • Records traceable evidence
  • Repeat and follow-up loops
View Cases
Success cases

Compressed air leak inspection

Through route-based acoustic inspections, invisible compressed air losses were converted into clear maintenance tasks.

  • Clear detection route.
  • Records traceable evidence
  • Repeat and follow-up loops
View Cases
Success cases

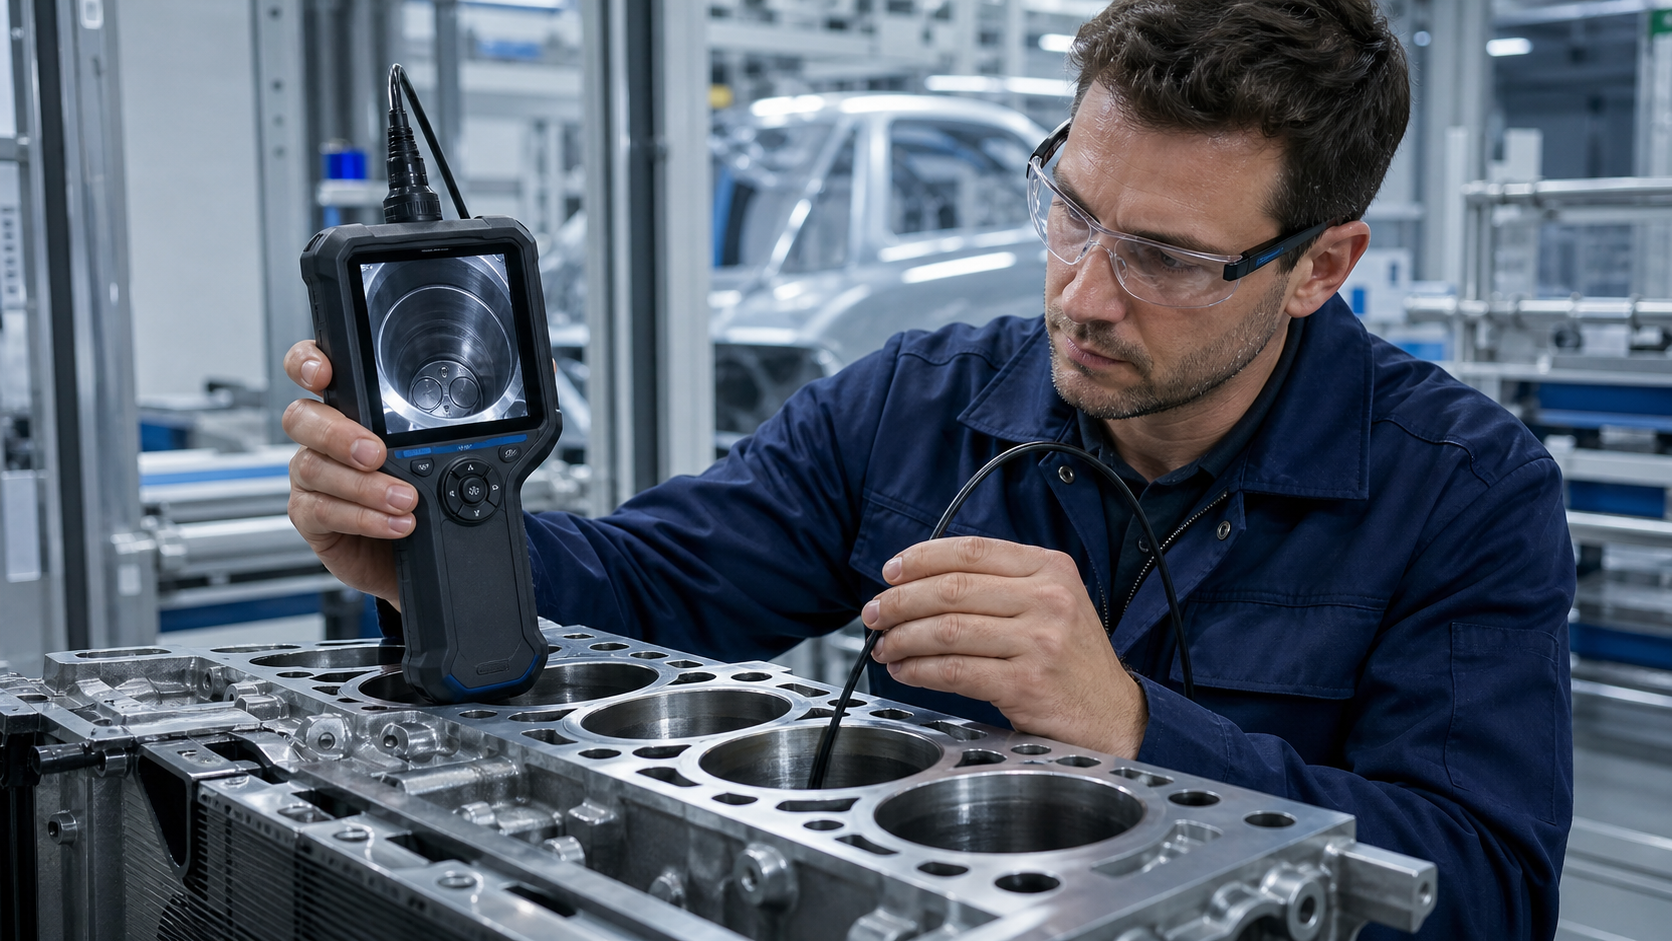
Vehicle engine cavity detection

Recording of the cask and internal surface state through visualization tests to provide a basis for maintenance decisions.

  • Clear detection route.
  • Records traceable evidence
  • Repeat and follow-up loops
View Cases
Success cases

Electrical equipment partial discharge screening

acoustic imaging helps field teams quickly screen switch equipment and prioritizes follow-up testing.

  • Clear detection route.
  • Records traceable evidence
  • Repeat and follow-up loops
View Cases
Success cases

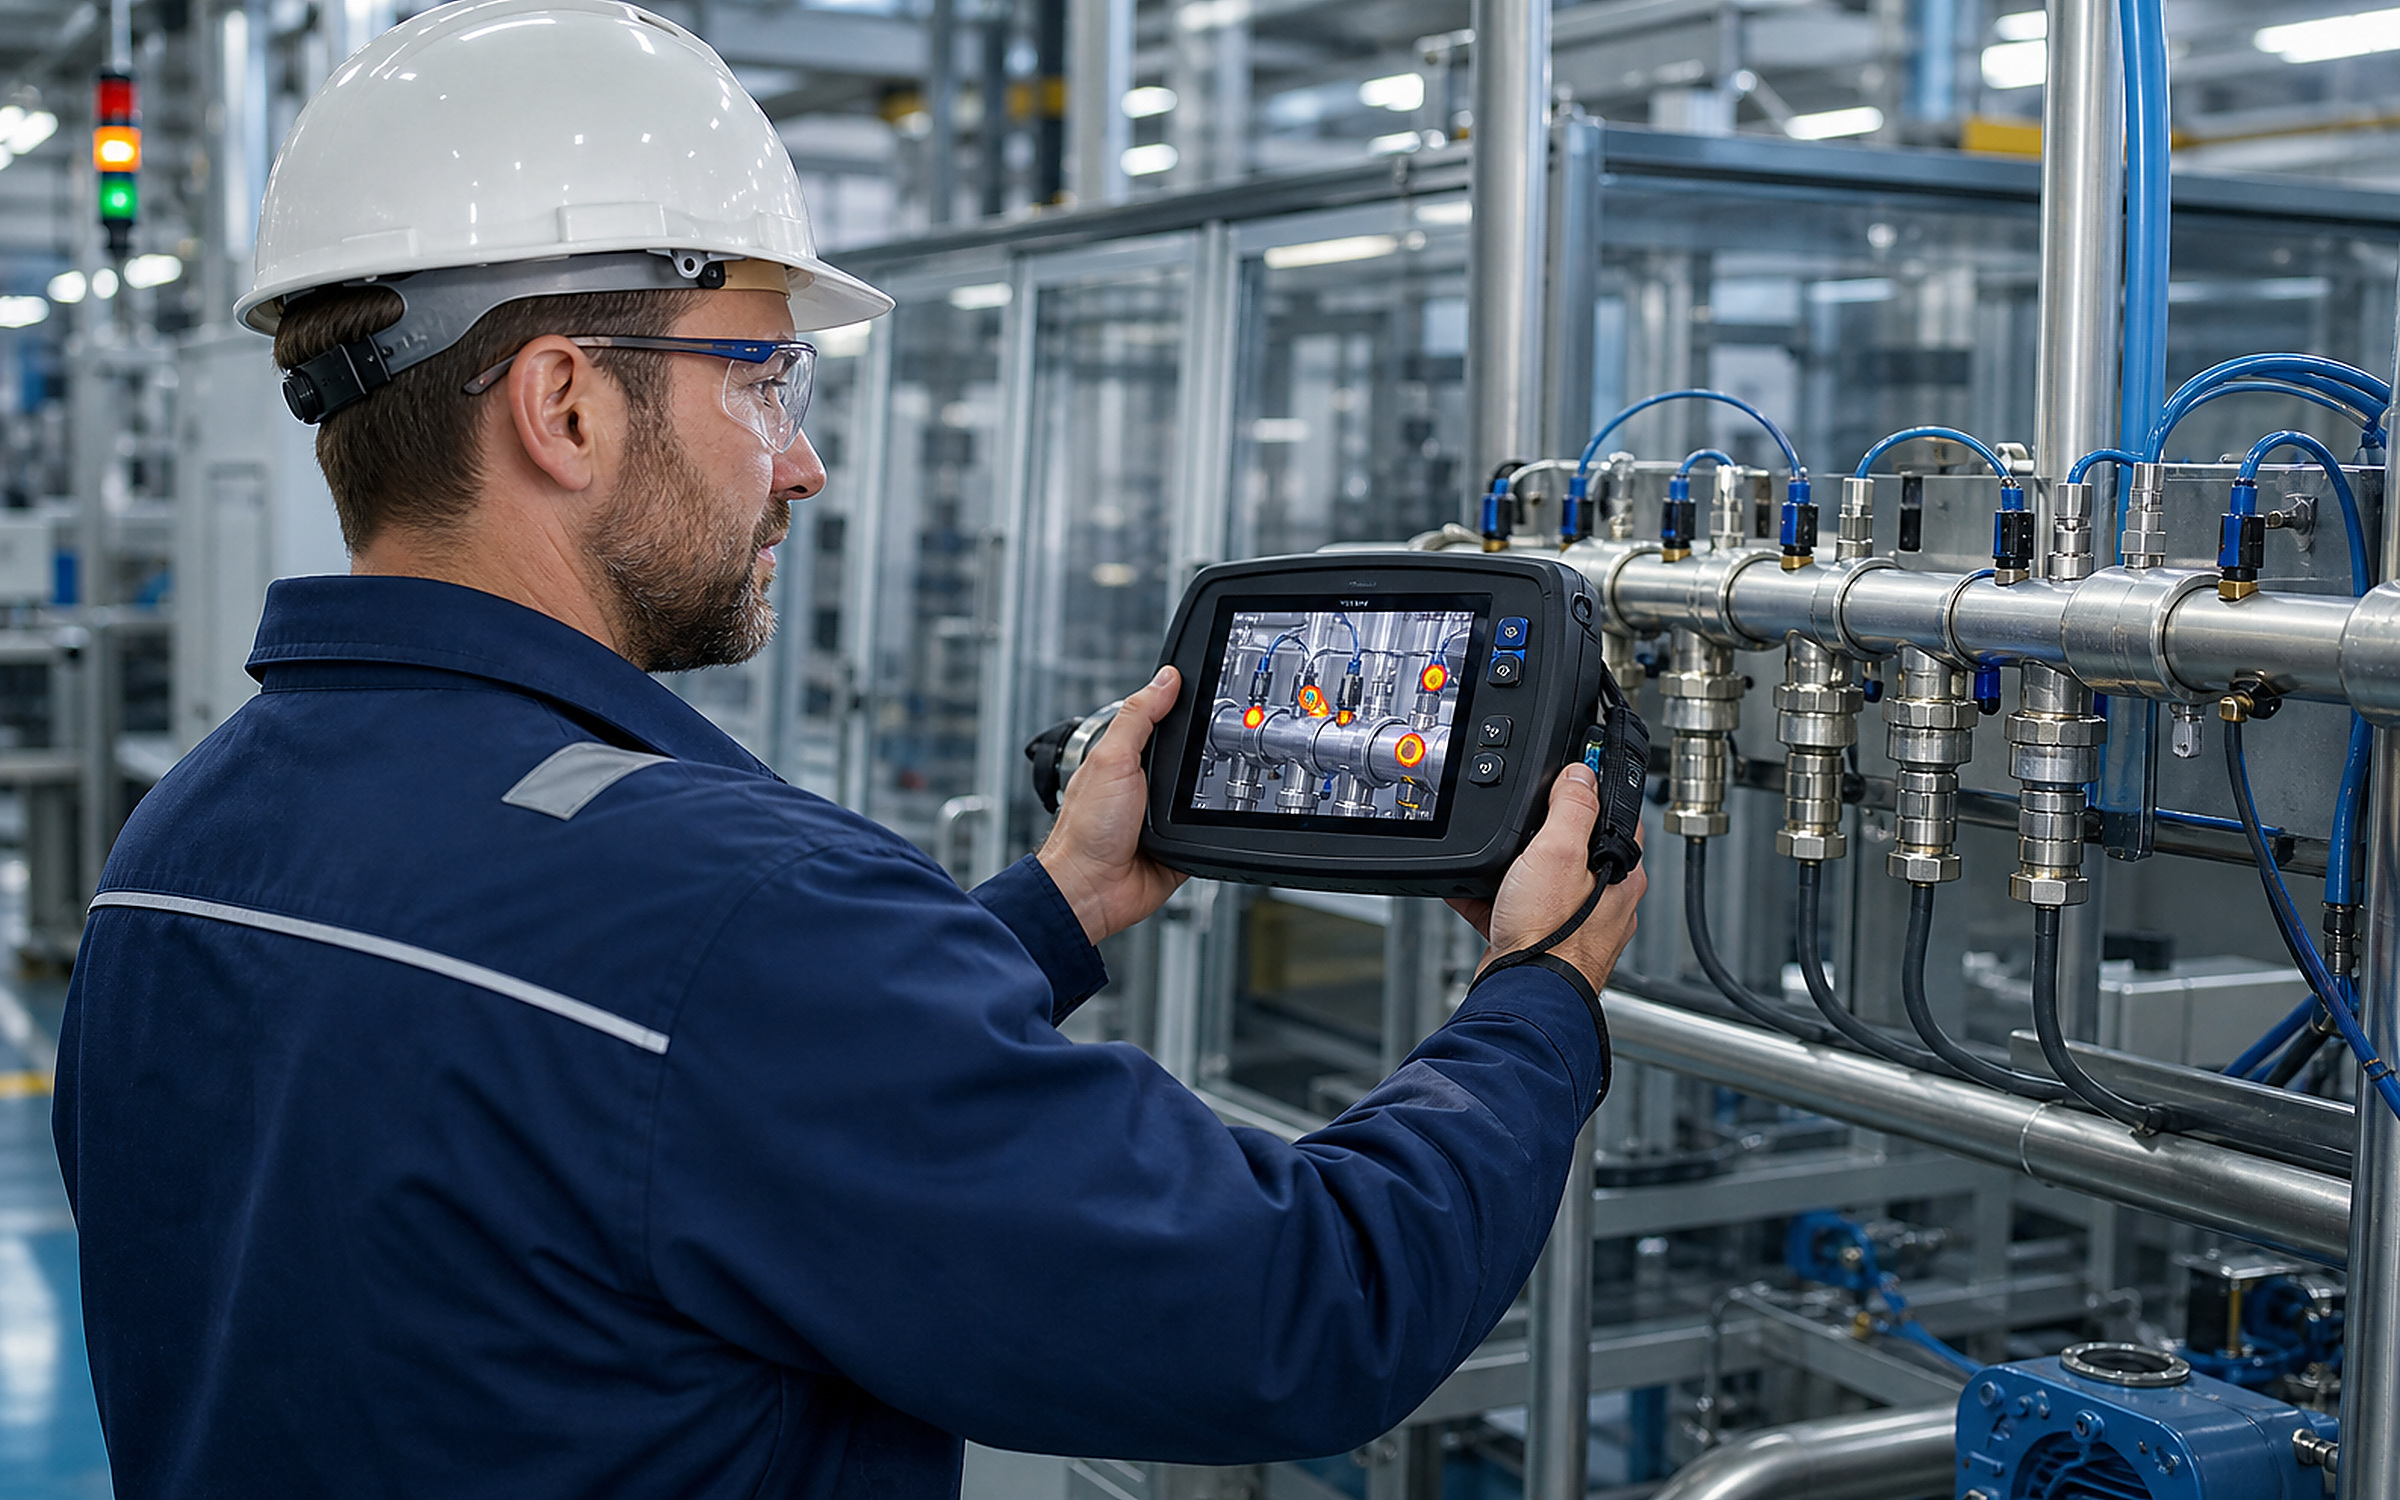
Pyrochemical pipe leak detection

Quick checks of valves, Franks and pressure connect points are conducted through non-contact acoustic inspections.

  • Clear detection route.
  • Records traceable evidence
  • Repeat and follow-up loops
View Cases
Success cases

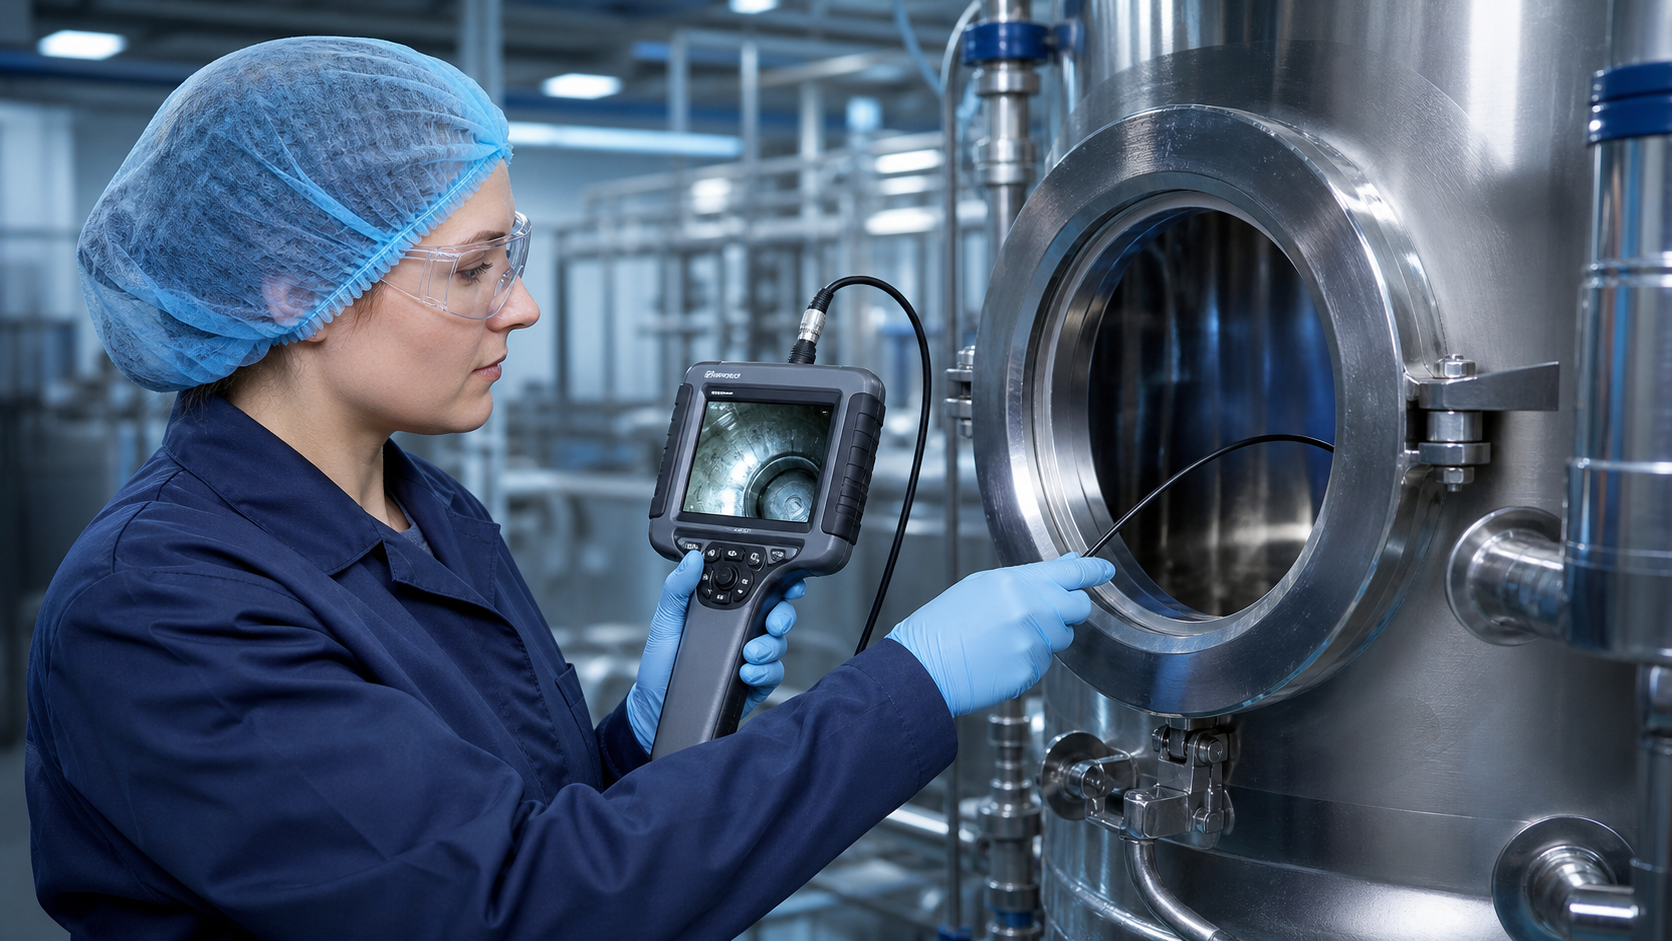
Internal detection of process containers

Remote visualization tests are used to inspect hard-to-reach stainless steel-process areas and to support health status reviews.

  • Clear detection route.
  • Records traceable evidence
  • Repeat and follow-up loops
View Cases
Success cases

Internal survey of small-calibre municipal pipes

The use of pipeline inspection borescope to observe the inner walls, interfaces and sediment state of the municipal small-calibre pipe, combined with video recording of the site location.

View Cases
Success cases

Internal detection of castings

Use industrial borescope to observe the inner cavity and interior wall surfaces of the casting, to record the internal structure and visible state, and to facilitate quality review.

View Cases
Success cases

Case of compressed air leak detection

A manufacturing plant used acoustic imaging camera to identify leakages, resulting in annual savings of more than Euro43,000.

  • Identification of detection challenges
  • Complete site testing
  • Validation of improvements
View Cases