Confirm conditions.
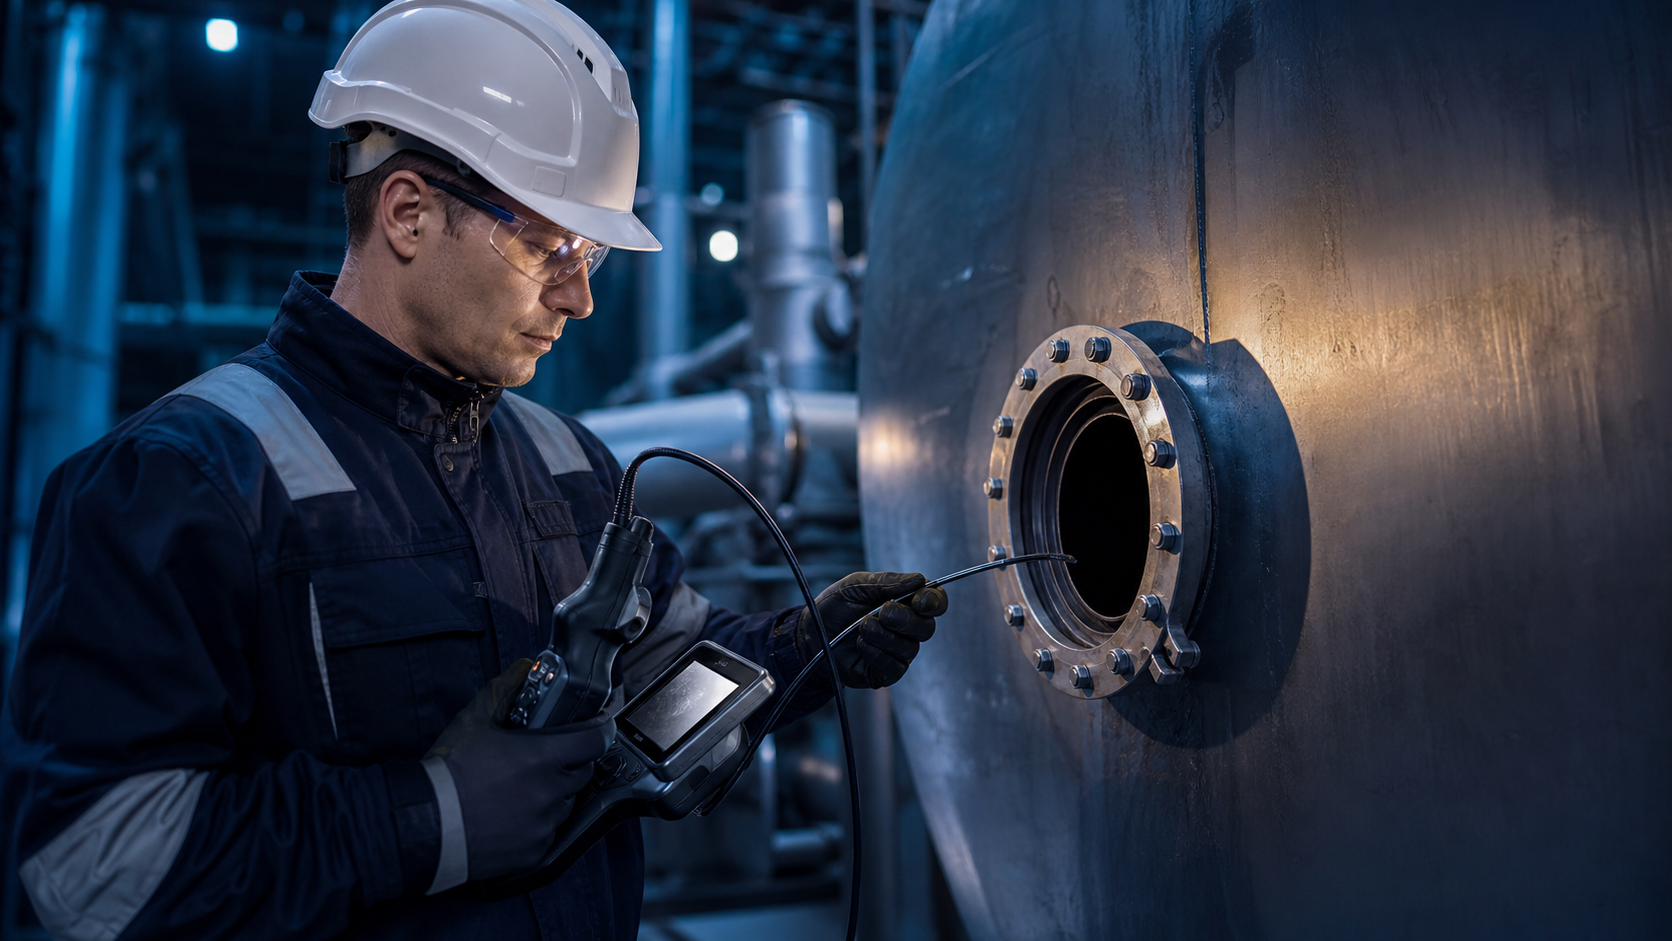
Prior to detection, the temperature range, liquid or chemical medium, the entrance diameter, the length of the path and the motor component risks need to be identified, and the probe protection and accessories selected according to the actual environment.
Ensure image quality
Maintaining optical end cleaning, lighting stabilization and controlling insertion processes will facilitate clear and comparable test evidence.
Industry background
The “high-resolution industrial borescope environmental requirements” typically relate directly to equipment reliability, production continuity, energy management or quality control.The temperature, medium, entry geometry and motor component risk should be identified prior to detection.At the industrial site, the single detection of anomalies does not amount to the completion of a test mission, but also requires the identification of the anomaly, recording of the operation, assessment of the impact range and transmission of the results to the maintenance and engineering team.Only when a closed ring is formed, from discovery, recognition to processing and retroactivity, can the detection work really be of value.
Establish a test plan
Before testing is carried out, lists of equipment, process processes and historical failure records should be compiled, and priorities should be based on risks, downtime effects and accessibility.Routes should cover key connecting points, rotation equipment, pressure systems and internal areas that are difficult to observe directly.For industrial borescope, clear access, length, diversion and lighting conditions are required;For acoustic imaging camera, background noise, distance, load and possible sources of interference need to be considered.
Regulate on-site records
The operator shall be the recorder device number, location, time, operational status and test parameters for each discovery, and shall maintain a panorama showing the environment and a proximate view showing details.The leakage, partial discharge or abnormal acoustic sources should be identified at different distances and angles;For internal cracks, corrosives, wear and tear, or foreign matter, the direction and size of the observation reference shall be recorded.Uniform naming rules can reduce the cost of subsequent search and communication.
Assessment and processing
The results should be graded according to safety, quality, energy loss and production impact.High-risk projects need to be scheduled for review and processing as soon as possible, and projects that can be completed in conjunction with planned downtime should be brought into the maintenance plan.Once the maintenance is completed, the same route and proximity parameters are re-measured to determine the effectiveness of the treatment and to provide comparable evidence for subsequent trend analysis.For findings that may not be identified at the moment, original data should be retained and reviewed jointly by the relevant professionals.
Continuous optimization of the inspection system
As records build up, the enterprise can gradually optimize the inspection cycle, spare parts arrangements and equipment retrofitting programme by analysing the problem position of the high frequency, repeat the cause of failure and maintenance effects.Standardized industrial inspection not only helps teams to detect problems earlier, but also reduces ineffective dismantling, shortens routing and improves inter-sectoral collaboration.The integration of test data into the asset management process will allow evidence on-site to sustain more reliable maintenance decisions.